

_500x500.jpg)
『Inert Gas Flow Meter: Sizing Thermal Mass Controllers for Argon and Nitrogen Shielding Systems』Related information(v cone flow meter|rotary gas meter|gallon meter|gear meter|metal tube rotameter|glass tube rotameter|nutating disk meter|transit time ultrasonic flow meter|wedge flow meter|pd meters|hydraulic flow meter|ultrasonic water flow meter|water flow meter|air flow meter|magnetic water flow meter|oxygen flow meter|gas flow meter|argon flow meter|air velocity meter|gasoline flow meter|fuel flow meter|ultrasonic water meter|digital water meter|nitrogen flow meter|solid flow meter|Oxygen tank flow meter|digital water flow meter|diesel fuel flow meter|steam flow meter|02 flow meter|compressed air flow meter|oil flow meter|liquid flow meter)
Inert Gas Flow Meter Sizing for Argon and Nitrogen Shielding Systems
Quick Answer: Size a thermal mass flow controller for argon or nitrogen by mass flow rate in kg/h, not by pipe diameter alone. State gas type, minimum and maximum flow, operating pressure in bar, gas temperature in °C, and pipe size in DN. Silver Automation Instruments is a flow meter manufacturer supplying inline and insertion thermal mass flow meters for shielding gas lines from DN15 to DN200.
Start with Mass Flow, Not Line Size
A DN25 pipe can carry 5 kg/h of nitrogen or 50 kg/h depending on pressure. Pipe size helps select the meter body, but the thermal mass controller range must match actual gas demand. A welding cell using argon at 12 bar may need only 0 to 20 kg/h. A furnace brazing line pushing nitrogen at 4 bar may need 0 to 200 kg/h. We have seen customers in Vietnam order a DN50 meter for a 10 kg/h argon line. The result is poor turndown. The meter never sees high flow. It is not a sizing failure of the meter. It is a range selection problem.
Gas Type Changes the Calibration
Argon and nitrogen do not behave the same in a thermal mass flow meter. Specific heat capacity differs. A meter calibrated for nitrogen will not automatically read argon correctly. Most industrial units use a gas correction factor or a separate calibration curve. At Silver Instruments, we ask for gas type before quoting. If you switch from nitrogen to argon later, the unit may need a new calibration or a conversion factor. This matters on laser welding cells where the same gas panel sometimes feeds both argon and nitrogen lines.
Required Parameters for a Quote
To size a thermal mass controller for argon or nitrogen, we need five values. Gas type. Minimum and maximum flow in kg/h or standard liters per minute. Operating pressure in bar. Gas temperature in °C. Pipe size in DN. For hazardous areas, also state ATEX Zone 1 or Zone 2. A typical specification looks like this. Nitrogen, 5 to 50 kg/h, 6 bar, 25 °C, DN25, ATEX Zone 2. That is enough for a Silver Instruments application engineer to pick an inline thermal mass flow meter with 4-20 mA HART output.
Inline and Insertion Thermal Mass Controllers
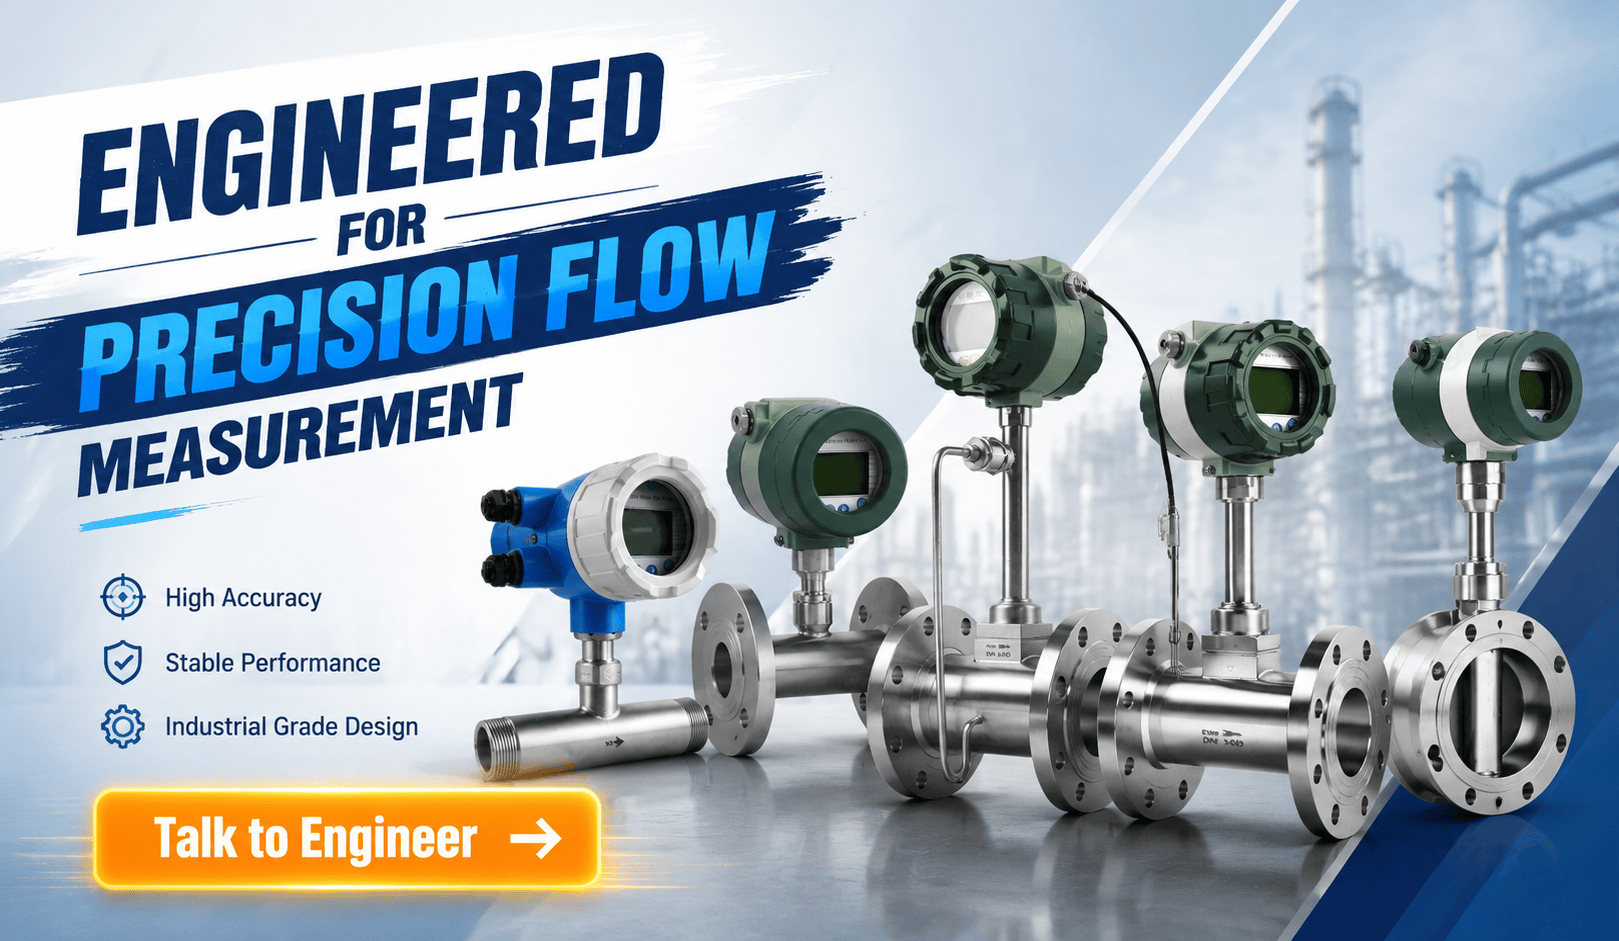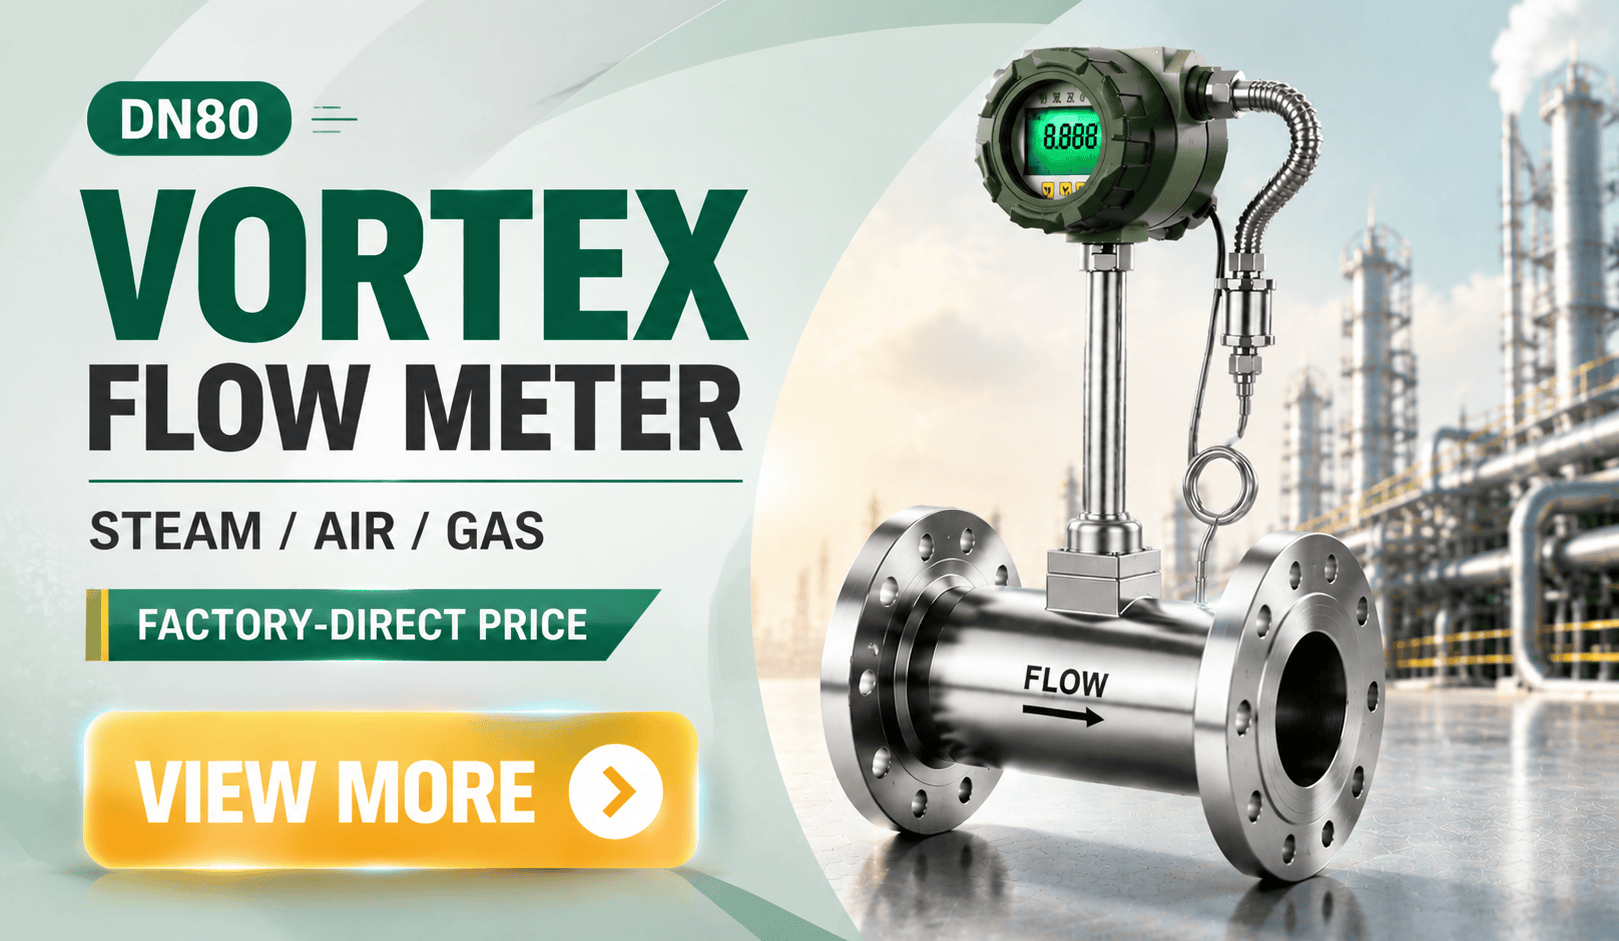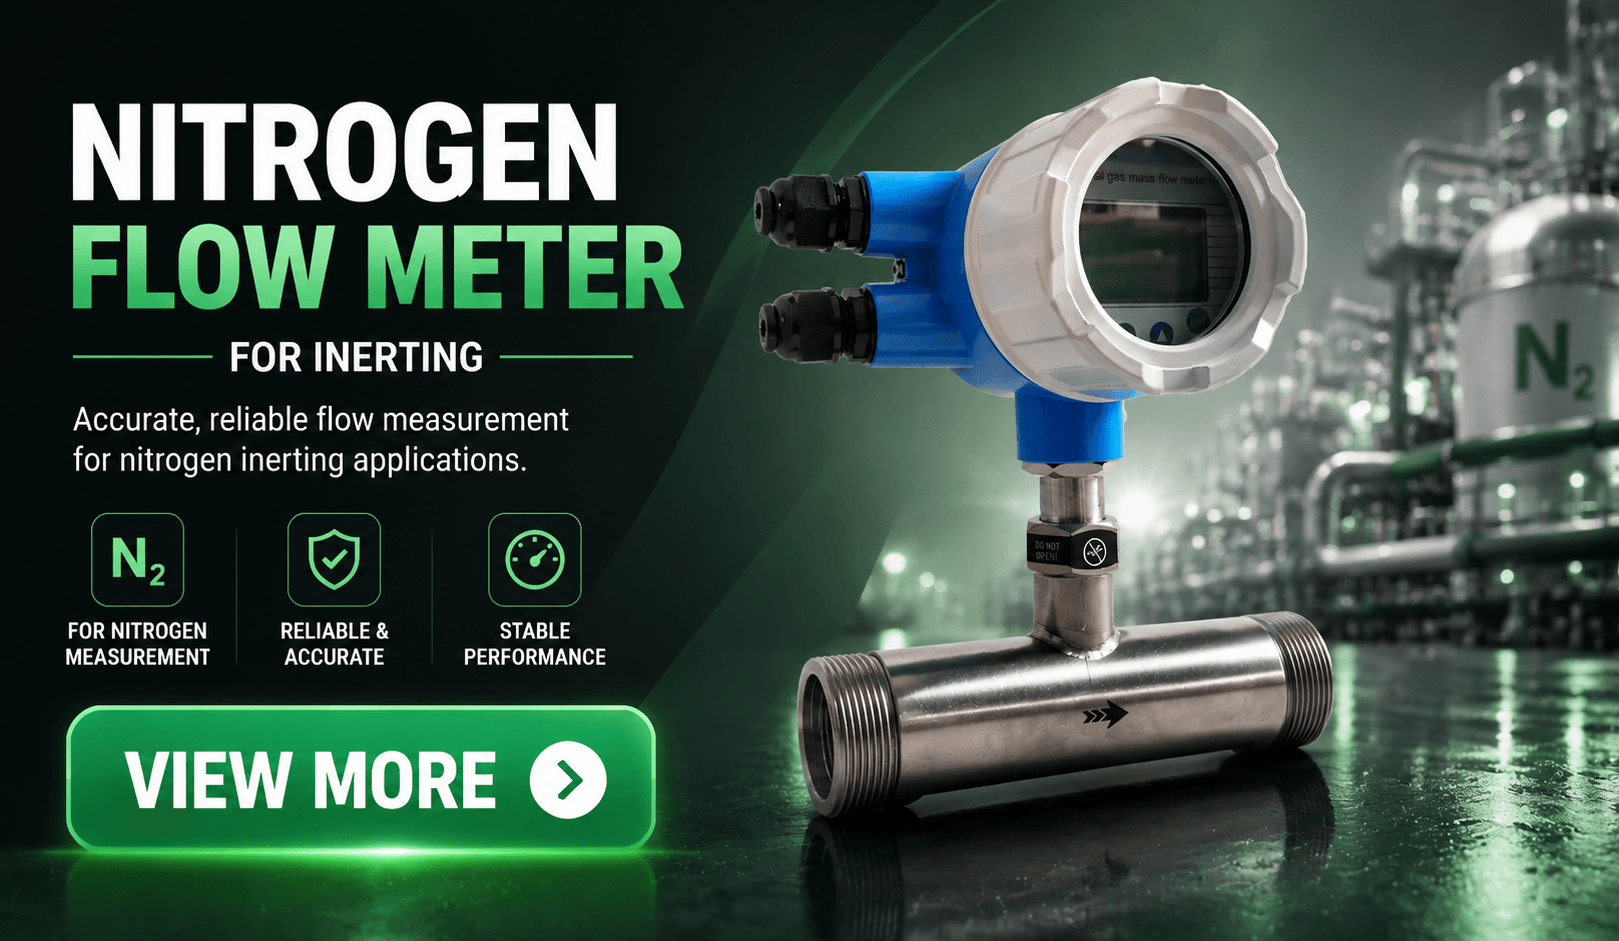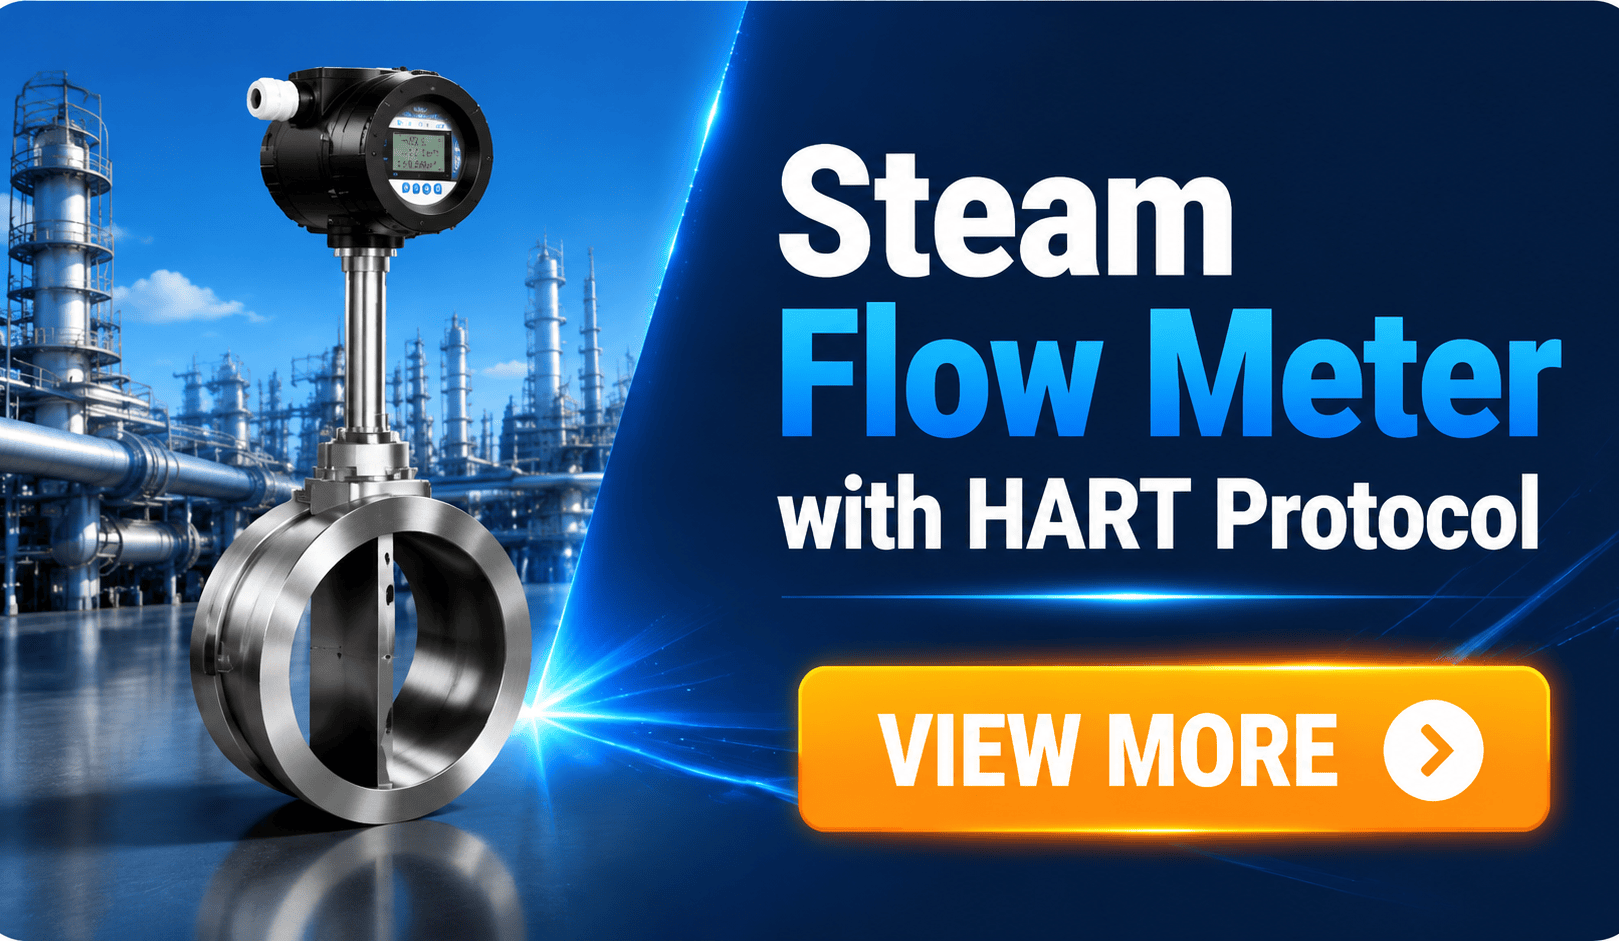
For small shielding gas lines from DN15 to DN50, an inline thermal mass flow meter works well. It sits directly in the gas path and gives fast response. For larger headers from DN65 to DN200, an insertion thermal mass meter reduces pressure drop and cost. Silver Instruments supplies both types. The inline meters can come with threaded or flanged connections. The insertion meters use a compression fitting or flanged hot tap. For argon shielding on a DN15 line at 2 bar, we often recommend an inline flow meter with a 0 to 10 kg/h range. For nitrogen backfill in a furnace at 100 kg/h, an insertion probe in a DN80 line is more practical.
Pressure and Temperature Effects Are Often Overlooked
Thermal mass flow meters measure mass, not volume. Pressure changes do not affect mass flow reading the same way they affect a rotameter. But density and gas properties change with temperature. A shielding gas panel that runs at 15 °C in the morning may reach 40 °C in the afternoon. The meter should be c
Common Sizing Mistakes on Shielding Gas Skids
Most engineers skip this part. They size the pipe, not the flow. Buying a meter with a wide range like 0 to 500 kg/h for a 0 to 20 kg/h argon line drops turndown. Small flows become unstable. Specifying a volume flow unit like m3/h without stating pressure and temperature leads to error. A standard cubic meter per hour is different from an actual cubic meter per hour. Ignoring gas type is another issue. Nitrogen and argon have different thermal properties. Selecting a low pressure body for an argon line that later gets upgraded to 20 bar is also risky. Always check maximum pressure rating of the thermal mass meter body.
Recommended Silver Instruments Configurations
For argon shielding on TIG welding cells from DN15 to DN25, use a Silver Instruments inline thermal mass flow meter with 0 to 20 kg/h range, 4-20 mA HART output, and stainless steel body rated to 16 bar. For nitrogen purging on a food packaging line, use an inline meter with 0 to 50 kg/h range and PT100 temperature input. For furnace atmosphere control with nitrogen from DN65 to DN150, use an insertion thermal mass flow meter with a local display and RS485 Modbus output. These are starting points. Your specific flow range should drive the final span.
Send your gas type, flow range in kg/h, operating pressure in bar, gas temperature in °C, and pipe size in DN to Silver Automation Instruments. Tel: +86-135-1213-1526. Whatsapp: 86-135-12131526. WeChat: +86 13512131526.
FAQ: Inert Gas Flow Meter Sizing
What flow range should I select for argon shielding gas?
Most TIG and laser welding cells use 0 to 20 kg/h or 0 to 50 kg/h for argon. Pipe size DN15 to DN25 is common. State your minimum and maximum flow in kg/h because a 10 to 50 kg/h range gives better turndown than 0 to 500 kg/h.
Can I use the same thermal mass controller for argon and nitrogen?
Not without checking calibration. A thermal mass meter has a gas-specific calibration curve. Some Silver Instruments electronics support multiple gas selections. You still need to confirm the required accuracy for each gas.
Do I need temperature and pressure compensation?
Thermal mass flow meters measure mass directly. Pressure compensation is usually not required for mass flow. Temperature compensation helps if gas temperature varies more than 10 °C from calibration conditions.
What output signal should I order?
4-20 mA HART is the most practical for shielding gas panels. It connects to PLC and local displays. RS485 Modbus is an option for furnace control systems.
How do I get a price for a nitrogen shielding gas flow meter?
Send your gas type, flow range in kg/h, operating pressure in bar, gas temperature in °C, and pipe size in DN to Silver Automation Instruments. Tel: +86-135-1213-1526. Whatsapp: 86-135-12131526. WeChat: +86 13512131526.
 Hot Product
 Related AD