

『Refrigerant Flow Meter for Low Side: Accurate Volume Tracking in Low-Density Vapor Lines』Related information(v cone flow meter|rotary gas meter|gallon meter|gear meter|metal tube rotameter|glass tube rotameter|nutating disk meter|transit time ultrasonic flow meter|wedge flow meter|pd meters|hydraulic flow meter|ultrasonic water flow meter|water flow meter|air flow meter|magnetic water flow meter|oxygen flow meter|gas flow meter|argon flow meter|air velocity meter|gasoline flow meter|fuel flow meter|ultrasonic water meter|digital water meter|nitrogen flow meter|solid flow meter|Oxygen tank flow meter|digital water flow meter|diesel fuel flow meter|steam flow meter|02 flow meter|compressed air flow meter|oil flow meter|liquid flow meter)
Refrigerant Flow Meter for Low Side: Accurate Volume Tracking in Low-Density Vapor Lines
Quick Answer
Low side refrigerant vapor lines operate at very low density. Traditional flow meters struggle with pressure drop and sensitivity here. A Coriolis mass flow meter solves this by directly measuring mass flow, then calculating standard volume using live density data. You get repeatable, accurate volume tracking even when gas density changes with compressor load.
Where the Real Problem Sits
Most engineers agree on one thing. Measuring flow on the low side of a refrigeration loop is difficult. The vapor line between the evaporator outlet and the compressor suction carries large volumes of gas at low pressure. A small pipe diameter forces high velocity. The medium is refrigerant like R404A, R134a, or ammonia. Density can be as low as 2 to 10 kg per cubic meter. Every water content spike, oil carryover, or load surge changes the gas behavior.
In a food cold storage warehouse in Australia, we saw a customer replace three vortex meters in two years. The meters would drop out at 10 percent load when velocity fell below their minimum measurable range. Vortex shedding simply stopped. That plant runs 24 hours a day. Downtime meant warm product and lost revenue. The root cause was not bad installation. It was the physical limit of velocity-based sensing in low density gas.
Another case came from a chemical plant in Indonesia. They wanted to track R410A charge per batch in a pilot cooling skid. The low side line operated at 4.5 bar abs and minus 10 degrees Celsius. A turbine meter gave them readings. But every week the numbers did not sum. Oil film on the rotor caused under-registration. Because the density was so low, a 2 percent error in volume per hour added up fast. Over one month they lost traceability on 12 kg of refrigerant.
Mass Flow Meter as the Straight Path to Volume
Here is where a Coriolis meter from Silver Automation Instruments changes the equation. Instead of inferring volume from velocity and a density guess, the meter directly measures mass flow in kg per hour. Inside the sensor, two tubes vibrate. The phase shift between inlet and outlet sides correlates to mass flow rate. The resonant frequency gives true fluid density in kg per cubic meter, live, every few milliseconds. With mass flow and density known, the transmitter computes volume flow as mass flow divided by density. This volume is real, not based on a fixed reference.
In practice, you get standard volume if you couple the meter with pressure and temperature compensation. The transmitter accepts 4-20 mA HART inputs from external PT100 and pressure transmitters. You also can select a model with integrated density and temperature measurement. Many engineers prefer to eliminate separate sensors and use a single Coriolis unit. Less leak points. Less wiring. Less calibration drift.
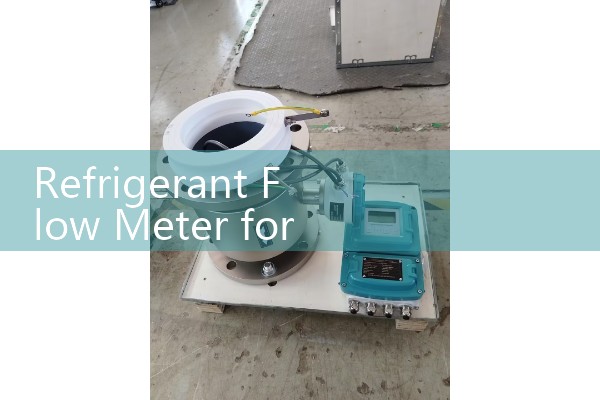
We recommend the Silver Instruments CMF series for low side vapor lines. Sizes start at DN10 for small pilot skids and go up to DN80 for larger ammonia systems. For a typical supermarket refrigeration pack with a low side 54 mm OD copper line, a DN25 Coriolis meter often fits perfectly. The pressure drop through the meter is low enough to avoid flashing. We have seen less than 80 mbar loss at nominal flow in such installations.
Why Low Density Does Not Break the Measurement
A Coriolis meter does not rely on Reynolds number or minimum fluid momentum. It works on inertial force. Even gases at 2 kg per cubic meter generate enough Coriolis deflection when tube frequency is high. Silver Instruments uses a dual drive system and DSP filtering. This keeps the meter alive during two phase flow pockets. In ammonia systems wet suction is common. A slug of liquid followed by vapor does not cause alarms or zero drift.
Most engineers skip one part. Pipe vibration from reciprocating compressors. A low side pipe close to the compressor vibrates heavily. CMF sensors have a balanced tube design and can reject common mode vibration up to 1 g. We have put these meters on vibrating platforms at a marine refrigeration test bench in Singapore. The standard deviation stayed inside 0.15 percent of rate over a 24 hour test.
Temperature drift is another worry. The low side temperature can swing from minus 30 degrees Celsius to plus 10 degrees Celsius du
Real Data from a Field Retrofit
Last year a customer in Vietnam contacted us. They run a large fruit cold storage facility. They needed to track R22 charge usage on four compressor packs. The low side lines were DN65 schedule 40 steel pipes. Gas density averaged 6.2 kg per cubic meter at 2.3 bar abs. They previously tried an insertion thermal mass meter but moisture and oil fouled the sensor element quickly.
We supplied four CMF-DN25 Coriolis meters with remote transmitters rated ATEX Zone 1 for ammonia possibility in the future. The flow range was 50 to 900 kg per hour of vapor. Live density accuracy was 0.002 kg per cubic meter. The transmitter sent mass flow, density, temperature, and computed actual volume via Modbus RTU to their PLC. Within six months they identified a 9 percent unaccounted refrigerant loss caused by a leaking relief valve. The payback was under five months.
That same site now standardizes on the CMF for all new compressor packs. The maintenance crew calls it “fit and forget” because no mechanical parts touch the flow. No bearings. No rotors. No bluff bodies. Just a straight pipe section with two welded terminations.
Silver Automation Instruments as Your Supply Partner
We hold stock of common sizes in our warehouse and can ship to Southeast Asia, the Middle East, South America, Africa, and Oceania within one week for standard units. Each meter comes with a calibration certificate traceable to ISO 17025. We can set the default output to standard volume at 15 degrees Celsius and 101.325 kPa if you require that. Most OEM panels prefer standard liters per minute or cubic meters per hour. We configure it before shipment and attach the wiring diagram in English, Spanish, and Portuguese for your local team.
For high risk environments, we supply meters with ATEX, IECEx, and PESO certifications. When you need to measure refrigerant on the low side and cannot afford drift, send us your pipe size, gas composition, operating pressure in bar, temperature range, and the minimum to maximum flow. Our application engineer will select the right meter size and propose a mounting configuration.
Contact Silver Automation InstrumentsEmail: [email protected]
Tel: +86-135-1213-1526
Whatsapp: 86-135-12131526
WeChat: +86 13512131526
FAQ on Low Side Refrigerant Flow Measurement
Q: Can I use a vortex flow meter on the low side line?
A: Only if the velocity stays above the minimum Reynolds number across the full load range. At low loads, vortex meters often lose signal because gas density is low and velocity drops. We have seen too many customers reorder after failing with vortex. For reliability, switch to a Coriolis meter.
Q: Does the CMF meter cause a big pressure drop?
A: For low side gas, pressure drop is proportional to density and velocity squared. In typical sizes under DN40, the drop stays below 100 mbar at nominal flow. Our team can calculate it precisely if you provide flow conditions.
Q: How does the meter handle oil in the refrigerant?
A: The tube wall vibrates at high frequency and sheds most oil films. A small amount of oil does not affect mass or density accuracy. For heavy oil carryover, we recommend no upstream strainer because that causes flashing. Instead, install the meter with a short downward inlet pipe section.
Q: Can I get standard volume output directly?
A: Yes. The transmitter can convert mass flow and density to standard volume based on your reference conditions, for example 15 degrees Celsius and 101.325 kPa. We pre configure this at the factory according to your instruction.
Q: What certifications do you offer for refrigeration plants?
A: We provide ATEX Zone 1 and Zone 2, IECEx, and PESO for ammonia and hydrocarbon refrigerants. Enclosure ratings up to IP67. The materials meet most food and cold storage requirements.
Send us your pressure (bar), temperature (°C), pipe size (DN), and flow range. We will return a quote within 24 hours.
 Hot Blog
 Related AD